CNC Nesting Workflow Optimization Guide for Panel Factories
A CNC nesting machine should be planned as part of a panel-production workflow, not selected from a headline speed or a generic specification table. The useful starting point is the factory’s actual board material, part mix, drawings, software, labeling method, downstream process and acceptance standard.
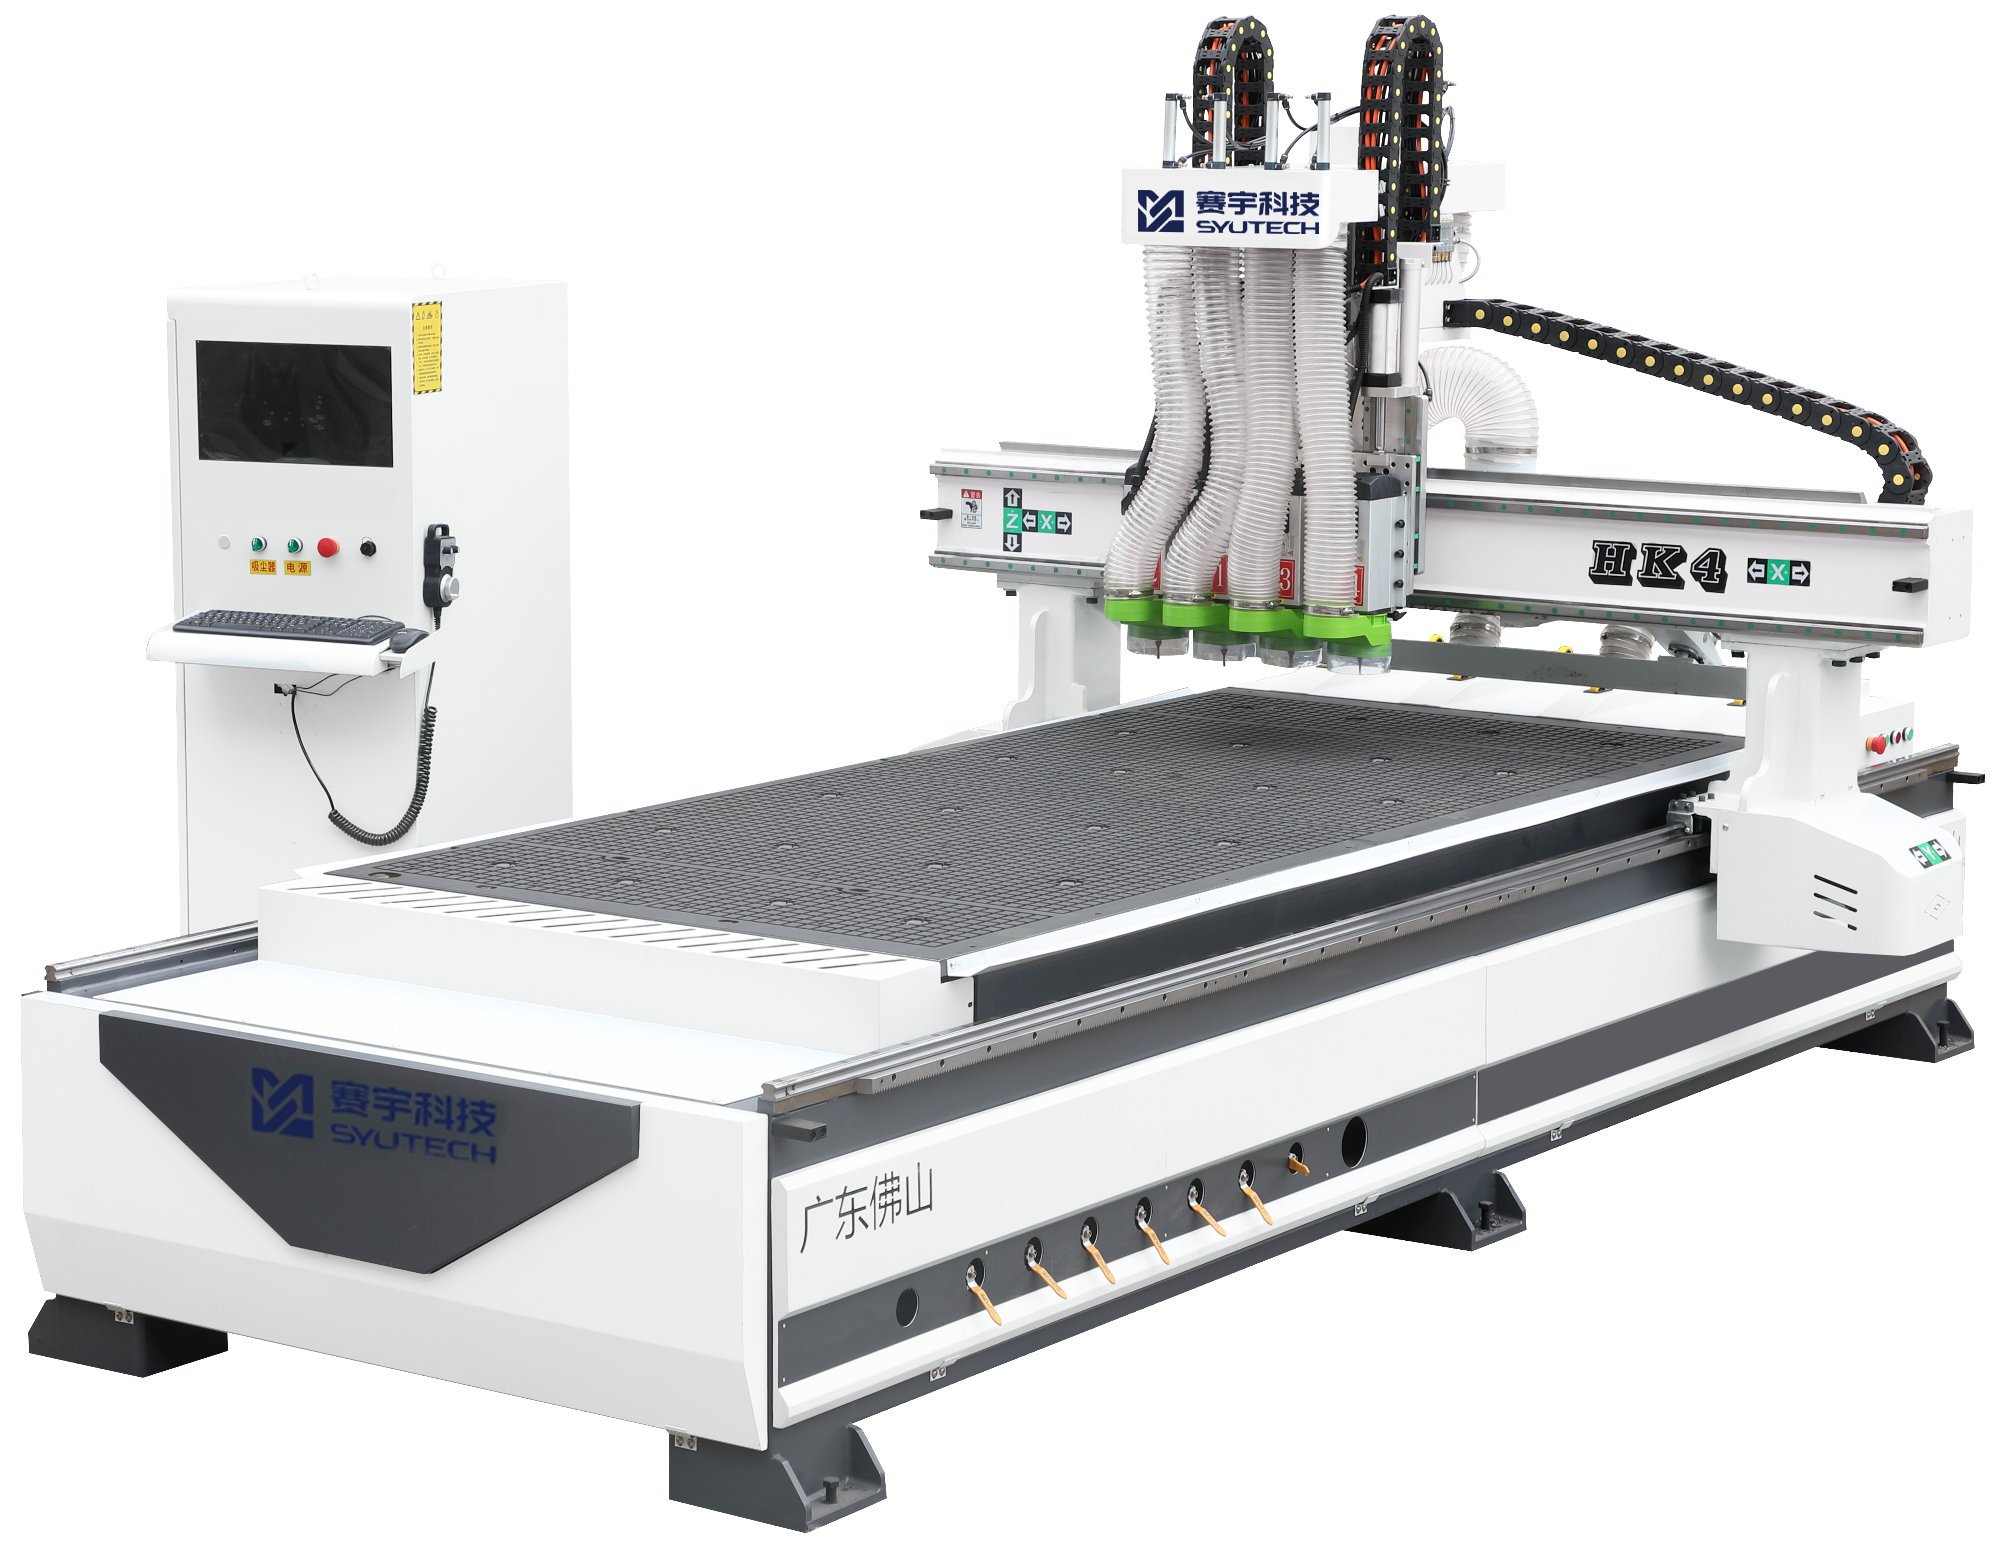
What the CNC Nesting Stage Must Deliver
In panel furniture production, the nesting stage prepares parts for edge banding, drilling, sorting and assembly. Depending on the confirmed machine configuration, the work may include panel cutting, routing, grooving, part identification and selected drilling operations. Buyers should verify each required operation against the proposed machine and tooling rather than assuming every nesting machine performs the same process.
Production Inputs to Prepare Before Comparing Machines
- Board materials, surface finish, common thicknesses and sheet sizes.
- Representative part drawings and a realistic order mix.
- Required cutting, routing, grooving and drilling operations.
- Current design, nesting, barcode and production-management software.
- Loading, unloading, labeling and part-sorting method.
- Dust-extraction interface, available floor space and material-flow direction.
- Downstream edge-banding, drilling and assembly requirements.
What Buyers Should Verify
| Verification area | Evidence to request |
|---|---|
| Workpiece compatibility | Sample processing using representative panels and part files. |
| Holding and table arrangement | Demonstration with the buyer’s panel sizes, cut layouts and small-part conditions. |
| Spindle and tooling | Tool list, process allocation and finished-edge inspection for the required materials. |
| Software workflow | File import, nesting, label, barcode and production-data demonstration. |
| Loading and unloading | Cycle observation that includes material handling rather than machining time alone. |
| Downstream handoff | Part identification and routing to edge banding, drilling, sorting and assembly. |
| Acceptance | Written criteria tied to the agreed sample, configuration and production conditions. |

CNC Nesting Machine or Beam Saw?
The choice depends on the production route. A beam saw is generally evaluated for straight cutting and batch panel-sizing work. A CNC nesting machine is generally evaluated when digital part files, mixed part sizes, routing or integrated data flow are important. Some factories use both processes. The decision should be based on order structure, part geometry, downstream requirements, labor and factory layout—not a universal claim that one machine is always better.
Vacuum, Tooling and Extraction Require a Real Test
Panel holding, tool selection and dust extraction interact with material type, part size, cut path and machine configuration. A buyer should include large panels, small parts, different surface materials and the intended toolpath in the sample test. Record movement, edge condition, dimensional results, dust removal and tool condition under the agreed test setup.
Connect Nesting to the Correct Downstream Process
Standard panel parts normally move from nesting to a suitable panel edge-banding process and then to drilling, sorting or assembly according to the factory route. Line-shaped mouldings and door-frame profiles are a different workpiece category and should not be treated as ordinary nesting output. Review the panel edge-bander guide and six-sided drilling guide for the relevant downstream stages.
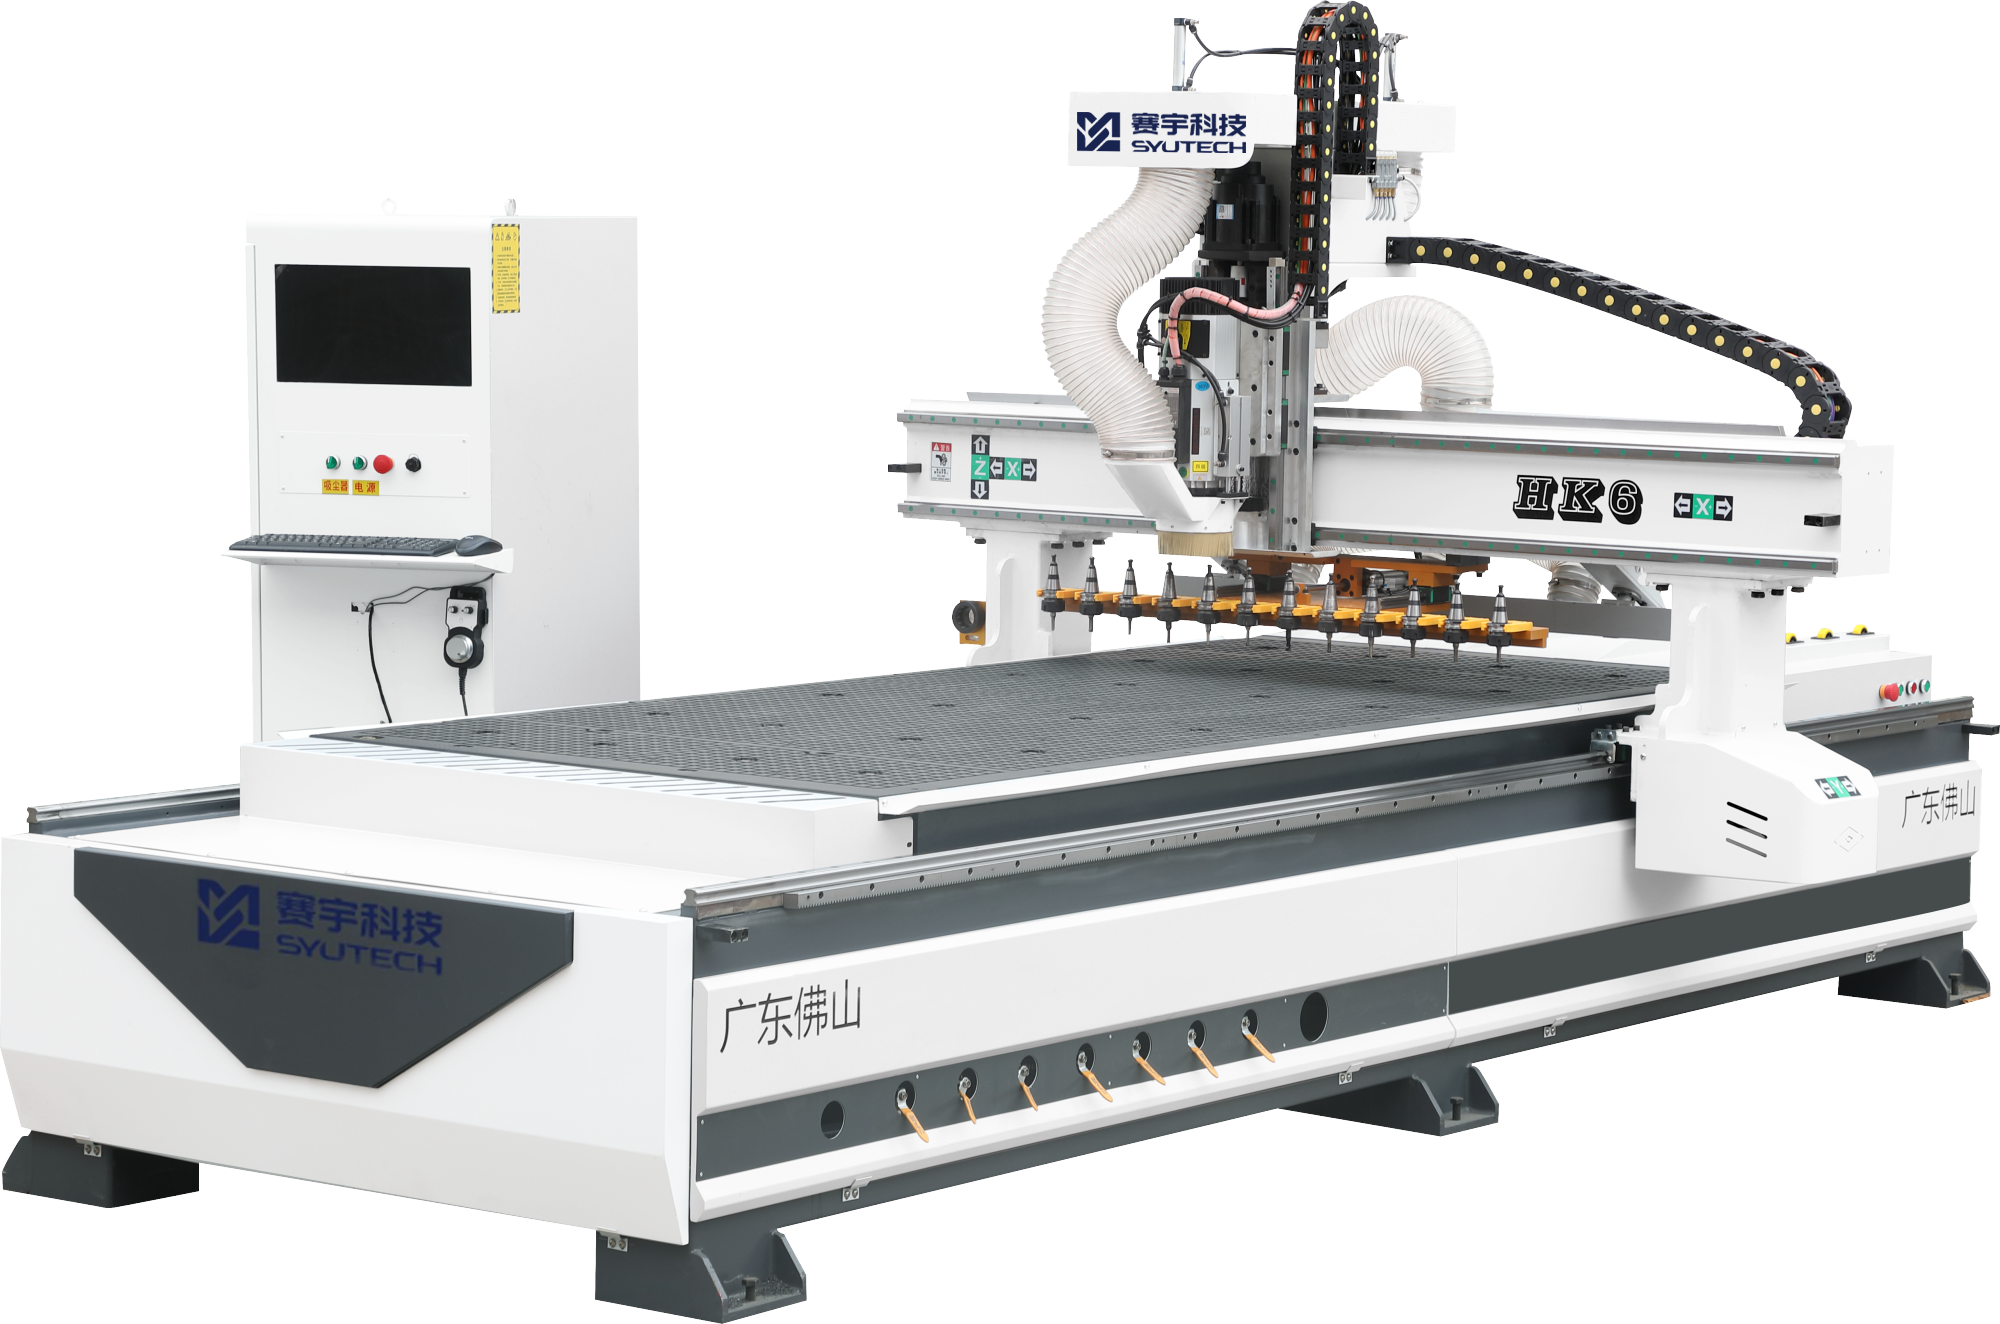
Recommended Sample-Test Record
- Identify each sample panel, material and part file.
- Record the proposed machine, tooling, software and holding setup.
- Observe the full route from file preparation through unloading and labeling.
- Inspect part dimensions, edge condition, grooves, holes and labels required by the process.
- Confirm which observations form part of the final acceptance agreement.
Frequently Asked Questions
What information should a buyer send first?
Send panel materials and sizes, representative part drawings, required operations, software workflow, production mix, factory layout and downstream process.
Can a catalogue specification confirm production performance?
No. A specification helps define the proposed configuration, but suitability should be checked with representative files, materials and an agreed sample test.
Should the fastest quoted cycle decide the purchase?
No. Compare the complete workflow, including file preparation, loading, holding, machining, labeling, unloading, sorting and downstream handoff.
Does every nesting machine include the same drilling capability?
No. Required drilling operations and tool layout must be confirmed for the proposed configuration.
Continue the Evaluation
- CNC nesting machine center
- CNC nesting machine selection guide
- Factory solutions and workflow planning
Send representative panel files, materials, required processes, software information and factory layout through the WMN contact page for a configuration and sample-test discussion.
Why One Good Sample Is Not Enough: First–Middle–Last Inspection for Decorative Profiles
Why Edge Banding First Changes Decorative Moulding Production
HK640 Crawler Edge Banding Machine
HK690 Narrow-Edge Banding Machine Overview